A cheese plant asks two opposite things of its air: pull moisture out of a hot, humid make room before it condenses overhead, and move a large airflow at very low velocity through ripening rooms where a few feet per minute change how much weight each cheese loses. Both demands, along with the packaging room’s need for filtered air moving outward, depend less on equipment capacity than on how the air is distributed. This article walks through each zone against FDA and USDA regulations and the ASHRAE Handbook, and explains what decides how a fabric duct performs.
U.S. regulations name the ducts
The FDA’s current good manufacturing practice rule requires a food plant built so that drip or condensate from fixtures, ducts and pipes does not contaminate food, food-contact surfaces or food-packaging materials (21 CFR 117.20(b)(4)). The U.S. Department of Agriculture adds room-by-room air requirements for dairy plants in 7 CFR Part 58. Across all three zones of a cheese plant, the common demand is that the air not become a source of contamination. In a 2022 warning letter to a cheese plant, the FDA described condensation water dripping from the ceiling and a fan vent onto shrink-wrapped cheese in a walk-in cooler.
Cheesemaking: latent load over open vats
Milk is pasteurized, coagulated in open vats, cut, cooked and molded. Pasta filata curd is stretched in water at 149 to 158 degrees Fahrenheit (65 to 70 degrees Celsius), and clean-in-place (CIP) runs at 158 F (70 C) or above (Tetra Pak, Dairy Processing Handbook). That heat and steam end up in the room air as latent load: moisture the system has to remove before it meets a surface below its dew point. ASHRAE’s Refrigeration volume (2010, Ch. 33) notes that cheese rooms normally open directly into the cheese-making room, where both temperature and humidity are quite high, and Ch. 22 warns that condensation on ceilings supports microbial growth and can drip onto product contact surfaces.
### No conventional duct belongs over an open vat
Galvanized sheet metal carrying cold air through a humid room runs with its skin below the dew point, so it sweats on the outside. Insulating it trades one problem for another: insulation that gets wet cannot be cleaned. Inside, neither galvanized nor stainless ductwork gets inspected, and in DUCTECOL’s field experience it is almost never cleaned. The regulation does not rule on materials; it requires that duct condensate stay off the food. What disqualifies conventional ductwork over a vat is the physics of a cold surface in saturated air.
Ripening: high airflow, low velocity
In ripening, cheese spends weeks or months in cold, very humid rooms, losing water and forming its rind. Parmesan stays about 14 months at 55 to 59 F (13 to 15 C) (ASHRAE Refrigeration, Ch. 33, Table 6), and Camembert ripens best at about 55 F (13 ± 1 C) and 94 ± 1 percent relative humidity (Leclercq-Perlat and colleagues, 2015). That weight loss is shrinkage, and every point of it is cheese that cannot be sold.
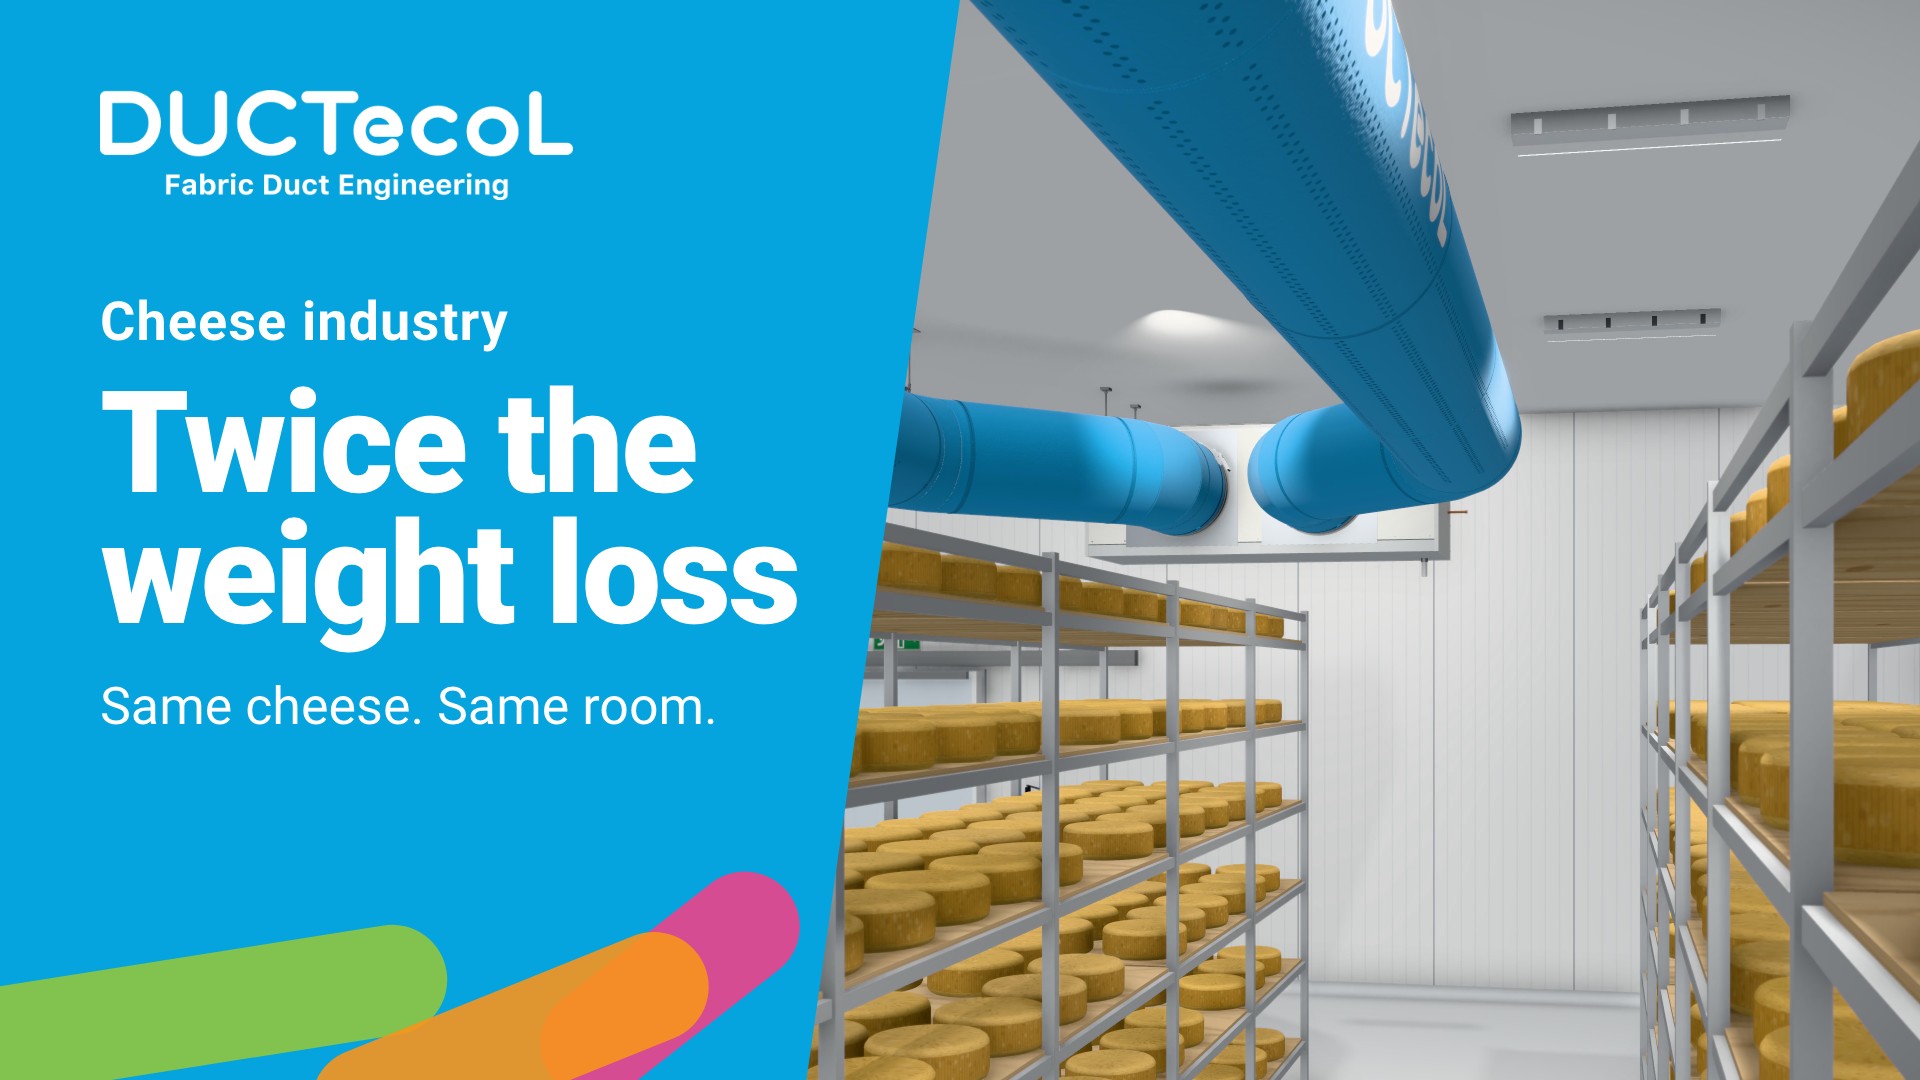
French research recommends an air velocity of about 20 fpm (0.1 m/s) around the cheese. Removing the water, however, takes a high recirculation rate: about 20 air changes per hour in the INRA pilot room (Mirade and colleagues, 2004). ASHRAE frames the target plainly: air circulation should only be enough to ensure uniform temperature and humidity throughout the room, and strong drafts cause uneven drying and cracking.
### The shrinkage equation
For the water term, Hélias, Mirade and Corrieu (2007) give:
dm/dt = −s · k · [a_w · p_sv(T_s) − rh · p_sv(T_∞)]
where dm/dt is the water lost per unit time, s the cheese’s exchange surface, k the water transfer coefficient, a_w · p_sv(T_s) the vapor pressure at the surface and rh · p_sv(T_∞) that of the room air. The set point fixes the bracket. The air reaching each cheese sets k, which triples between about 10 and 100 fpm (0.05 and 0.5 m/s), according to Mirade and colleagues (2004).
### Position in the stack decides
In an industrial raclette ripening room held at a single set point, shrinkage ranged from 4.1 to 8.7 percent of initial mass. Local velocity, from about 12 to 94 fpm (0.06 to 0.48 m/s) depending on distance to the ducts, had the greatest effect, and the top racks lost the most (Corrieu and colleagues, 2018). At the other extreme, in a room tested in France, the central stack right under the duct was left almost unventilated and local relative humidity peaked at 97 percent (Mirade, 2007). On Camembert, the white coat disappears if room humidity stays above 95 percent for as little as two or three days.
The industry pays twice. Producers move cheeses around the room to even out shrinkage, and ventilation accounts for 50 to 55 percent of total ripening costs (Mirade and colleagues, 2011). Tetra Pak adds that distribution ducts are difficult to keep free from mold and must be designed to allow cleaning and disinfection.
Packaging and shipping: filtered air moving outward
Cutting, grating and packaging form the most sensitive zone. In a semi-hard cheese plant, statistical analysis showed that air was the main source of the key contaminating molds, especially in the wrapping room (Kure and colleagues, 2004). USDA calls for filtered air and outward air movement in packaging rooms (7 CFR 58.411 and 58.413), and the FDA, in its 2017 draft Listeria guidance, recommends positive pressure for the ready-to-eat area. In the shipping cooler, adequate air circulation is required at all times, with evaporator condensate kept under control (7 CFR 58.126(e)(1)).
Fabric duct, zone by zone
In the make room, a fabric duct delivers treated air along the full length of the room at low velocity, so steam is carried off before it condenses over the vats, in line with the FDA’s recommendation to consider how airflow affects condensation. The duct itself does not condense. ASHRAE’s HVAC Applications volume (2019, Ch. 58) explains that a slightly permeable material allows air below dew point to be dispersed without condensation forming on the fabric system.
In ripening rooms, the reference studies were run with fabric ducts, and they show that fabric duct design decides uniformity. In Mirade’s CFD model (2007), at the same airflow, 3 mm (about 1/8 in.) orifices produced up to 60 fpm (0.3 m/s) around the cheese, while 20 mm (about 3/4 in.) orifices reached 120 fpm (0.6 m/s). DUCTECOL sizes each discharge for the exact position of each stack.
For hygiene, the fabric duct is taken down, washed, disinfected and verified outside the plant, with a report for each unit. ASHRAE’s Refrigeration volume (Ch. 22) lists washable fabric ducts designed and approved for such use as an option for easy cleaning. Inside a cold room it needs no insulation, because room temperature equals supply temperature.
CFD before fabrication
DUCTECOL models every project in computational fluid dynamics (CFD) to see how air will reach each stack, vat and packaging line before anything is cut. Manufacturing is high-tech, with shipping to more than 30 countries. Field measurement confirms the result.
Frequently asked questions
Will a fabric duct sweat when it carries cold air through a humid make room?
No. A DUCTECOL fabric duct does not condense, so it does not drip onto the product zone. ASHRAE’s HVAC Applications volume (2019, Ch. 58) attributes this to material permeability: a slightly permeable fabric can disperse air below dew point without condensation forming on the system. Galvanized sheet metal, by contrast, sweats on the outside and has to be insulated.
What air velocity should reach the cheese in a ripening room?
French research recommends about 20 fpm (0.1 m/s) around the cheese. ASHRAE asks for circulation that is only enough to keep temperature and humidity uniform and warns that strong drafts cause uneven drying and cracking. The challenge is holding that velocity while recirculating around 20 air changes per hour, which is why outlet design matters more than total airflow.
Why do the top racks of a stack lose more weight?
Because air does not reach every level of a stack at the same velocity. In the industrial raclette room studied by Corrieu and colleagues (2018), local velocity ranged from about 12 to 94 fpm (0.06 to 0.48 m/s) with distance to the ducts, higher velocity meant more weight loss, and the top racks showed the highest shrinkage. Sizing each discharge for the position of each stack addresses the cause rather than moving cheeses by hand.
Which U.S. regulations govern air and ductwork in a cheese plant?
FDA’s 21 CFR 117.20(b)(4) requires that drip or condensate from fixtures, ducts and pipes not contaminate food, food-contact surfaces or packaging. USDA’s 7 CFR Part 58 calls for filtered air with outward movement in packaging rooms and adequate air circulation at all times in coolers. FDA’s 2017 Listeria guidance, still a nonbinding draft, also recommends positive pressure in ready-to-eat areas.
How is a fabric duct kept clean in a dairy plant?
It is taken down, washed, disinfected and verified outside the plant, with a report for each unit that documents every cycle. That answers Tetra Pak’s requirement that ducts be designed to allow cleaning and disinfection, and ASHRAE lists washable fabric ducts as an option. The plant’s sanitation program sets the frequency.
In a cheese plant, the design question is not how much air the equipment moves but how that air reaches each cheese: latent load carried off the make room with no cold surfaces sweating over the vats, low and even velocity at every stack in ripening so shrinkage does not depend on position, and filtered air moving outward in packaging. Ductwork that does not condense, comes down to be washed, and has its discharges modeled in CFD for each stack meets those conditions; field measurement confirms it.
Planning or expanding a cheese plant? Request zone-by-zone fabric duct sizing with CFD modeling at fabricduct.co.